Industrial Weld Repair vs. Component Replacement: How to Make the Right Call
A cracked vessel shell, a corroded nozzle weld, or a worn shaft does not automatically mean a component has reached the end of its life. In many cases, a properly executed weld repair returns damaged equipment to safe service for a fraction of the cost and lead time of a new part. In other cases, repair only delays a failure that replacement would have prevented. The right call depends on what the damage actually is, whether a code-compliant repair path exists, and whether the finished repair can be verified before the component goes back into service. This guide walks through how plants and fabricators typically make that call, what the codes governing pressure equipment and piping require, and how testing and inspection remove the guesswork.
What Determines Whether to Repair or Replace an Industrial Component?
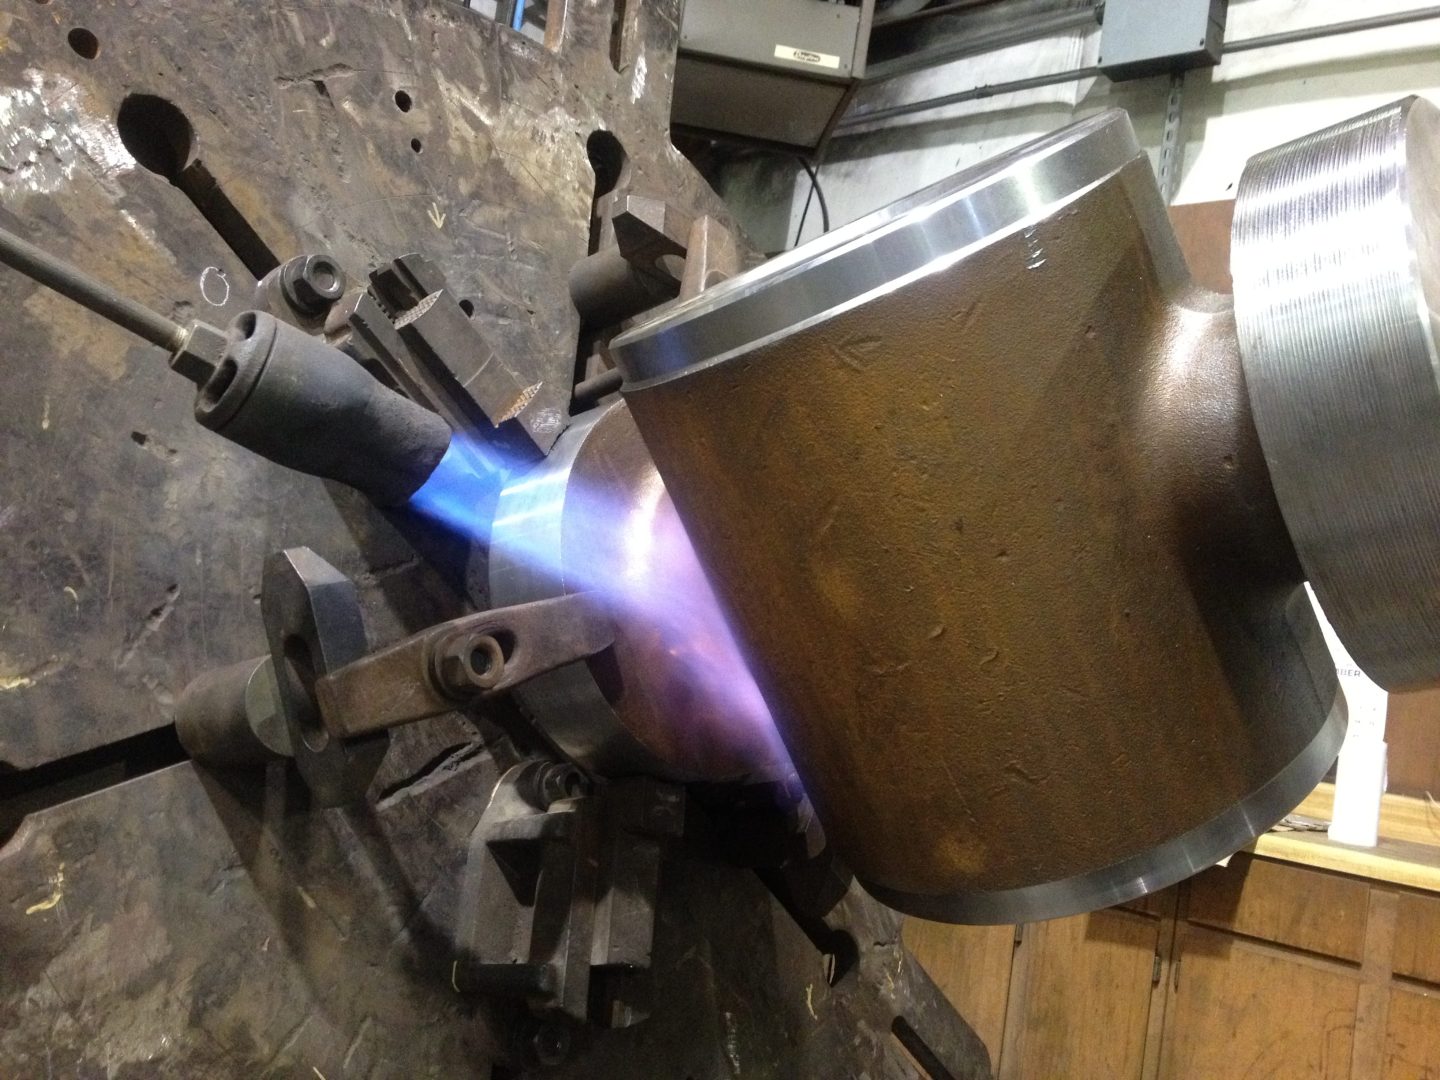
The repair-or-replace decision comes down to five factors: whether damage is localized or has compromised the base structure, whether a repair can restore the component to its original design conditions, the real cost and lead time of each option, whether the same failure has happened before, and whether the finished repair can be verified through testing before the equipment returns to service. No single factor decides it alone.
Repair is usually the right call when:
- The damage is confined to a weld, a wall-thinned area, or a localized crack in an otherwise sound structure
- A qualified welding procedure exists, or can be qualified, for the material and service conditions
- Repair cost and downtime are meaningfully lower than sourcing, installing, and requalifying a new component
- The component still has meaningful service life ahead of it
Replacement is usually the right call when:
- The base metal or structure itself is compromised, not just a localized area
- The same failure has recurred more than once in the same location
- The damage exceeds what the governing inspection code allows for repair
- A newer component would deliver a meaningful gain in safety, capacity, or reliability
When Does Weld Repair Make Sense for a Damaged Component?
Weld repair generally makes sense when damage is confined to a wear surface, a corroded section, or a localized crack in an otherwise sound component, and when a qualified welding procedure exists for the base material and service conditions. It works best when repair cost and downtime are clearly lower than sourcing, installing, and requalifying a new part, and when the component still has meaningful service life ahead.
This covers a wide range of situations: building up a worn bore before remachining, overlaying a corroded shell section, repairing a cracked structural frame, or restoring a damaged nozzle-to-shell weld on a vessel. Many maintenance and reliability teams treat repair as the default option once it clears roughly half to sixty percent of full replacement cost, as long as the technical case holds up. Cost alone should never override a technical no-go; a cheap repair that will not hold is not actually cheap.
When Should a Component Be Replaced Instead of Repaired?
Replacement is usually the better call when the base structure itself is compromised rather than just a localized area, when a component has failed and been repaired in the same location more than once, when the damage exceeds what the governing inspection code allows for repair, or when a newer component would deliver a meaningful gain in safety, capacity, or reliability that a repair cannot match.
A repeat failure at the same location is a signal worth taking seriously. It usually means the previous repair addressed the visible damage without correcting what caused it, whether that is a corrosion mechanism, a material mismatch, or a load the component was never designed to carry. Extensive cracking, severe porosity, or damage that has spread beyond a single localized area is also a strong indicator that repair is not the more economical path once engineering review, procedure qualification, and possible post-weld heat treatment are factored in alongside the welding itself.
What Do the Codes Governing Pressure Equipment and Piping Say About Weld Repairs?
For pressure vessels and process piping, the weld repair versus replacement decision is not purely a maintenance call. It falls under in-service inspection codes: API 510 for pressure vessels, API 570 for process piping, and, in most U.S. jurisdictions, the National Board Inspection Code (NBIC). These codes distinguish a repair, which restores equipment to its existing design conditions, from an alteration, which changes them, such as adding a nozzle or increasing the maximum allowable working pressure. Both classifications generally require an Authorized Inspector’s concurrence before the work is accepted.
The accepted repair methods themselves, weld buildup, insert plate, and full encirclement sleeve among them, are described in ASME PCC-2, Repair of Pressure Equipment and Piping, which is referenced directly by API 510, API 570, and the NBIC. Structural components that do not hold pressure, such as frames, supports, and housings, generally fall under a different set of standards rather than API or NBIC, so the applicable code depends on what kind of component is actually being repaired.
What Does a Weld Repair Actually Cost Compared to Replacement?
A weld repair quote is usually easy to compare against a new part’s purchase price, but that comparison misses most of the real cost of replacement. Rigging the old component out and the new one in, foundation or support modifications, requalification, and the downtime stacked on top of procurement lead time routinely add far more to a replacement than the new equipment itself costs.
Repair has its own hidden costs when it is done without a full picture of the damage. A repair that treats the visible symptom without confirming the root cause can fail again within months, which means the downtime and cost show up twice instead of once. When a repair quote starts approaching the same fifty to sixty percent threshold mentioned earlier relative to full replacement cost, that is usually the point to take a harder look at whether replacement is actually the cheaper path over the life of the asset.
How Do You Verify a Weld Repair Will Hold Before Returning It to Service?
A weld repair is only as good as the inspection behind it. Visual testing catches surface issues like undercut or a poor weld profile, while ultrasonic, magnetic particle, and liquid penetrant testing confirm that the repair does not carry embedded flaws, indications, or a heat-affected zone that will crack in service. Repair welding should also follow a qualified welding procedure specification, not field judgment alone.
WH Labs offers weld repair analysis alongside in-house non-destructive testing across visual, ultrasonic, magnetic particle, and liquid penetrant methods, so a repair can be verified against the same standards used to qualify the original weld procedure before the component goes back into service.
Why Root Cause Matters Before Choosing a Repair Method
A technically sound weld repair can still fail again if it addresses the visible damage without correcting what caused it. Corrosion concentrated at a weld’s heat-affected zone, a material that was never suited to the service environment, or inadequate post-weld cleaning are common root causes that a repair alone will not fix. Metallurgical testing and failure analysis identify the actual cause before a repair method is chosen.
A common pattern in pressure equipment repair is pitting or cracking that reappears at the boundary between the original weld and a repair weld within months of returning to service. Investigation often traces that back to heat-related changes in the original weld’s microstructure combined with incomplete post-weld cleaning, not a flaw in the repair method itself. WH Labs’ failure analysis services exist to catch that kind of root cause before a second repair repeats the same mistake.
How WH Labs Supports the Weld Repair vs. Replacement Decision
WH Labs supports the repair-or-replace decision with the same in-house capabilities used to execute the repair: weld repair analysis, non-destructive testing, and metallurgical failure analysis, backed by ISO/IEC 17025:2017 accreditation and ASME U and U2 stamps. That means the lab that determines whether a repair will hold can also execute the welding and fabrication work itself, without the job moving between separate vendors.
This matters most for clients in oil and gas, chemical processing, and power generation, where a damaged pressure vessel, pipe, or structural component needs an answer that holds up under inspection, not just a welder’s best guess. WH Labs’ welding and fabrication team can carry out the repair once testing confirms it is the right path forward.
Frequently Asked Questions
Is a weld repair as strong as the original component?
When it is performed to a qualified welding procedure and verified with non-destructive testing, a weld repair can restore a component to its original design conditions or close to them. The result depends on whether the correct filler material, preheat, interpass temperature, and post-weld cleaning were used, not on whether the fix was a repair rather than a replacement. A poorly executed repair on a new part can end up weaker than a well-executed repair on an aging one.
How much cheaper is weld repair than component replacement, generally?
Weld repair often costs a fraction of full replacement once the total replacement bill, including procurement, rigging, requalification, and downtime, is counted rather than just the price of the new part. Many maintenance teams treat repair as the default option as long as its cost stays meaningfully below replacement and the technical case supports it, though the exact savings depend on the component, the damage, and the industry.
Can a pressure vessel or process pipe be weld repaired, or does it have to be replaced?
Most localized damage on pressure vessels and process piping, such as thinning, isolated cracking, or a damaged nozzle weld, can be weld repaired under API 510, API 570, or the NBIC using accepted methods from ASME PCC-2. Replacement becomes necessary when the damage exceeds what those codes allow for repair, when the base structure itself has failed, or when an Authorized Inspector determines the equipment cannot be safely returned to service through repair.
How do you know if a weld repair is going to fail again?
Repeat failure at the same location is usually a sign that a previous repair addressed the visible damage without correcting its root cause, such as a corrosion mechanism, a material mismatch, or a welding procedure that was not suited to the service conditions. Metallurgical testing and failure analysis identify that root cause so the next repair, or the decision to replace instead, actually resolves the problem rather than sending the component back into service to fail again.
What information does a testing lab or welding shop need before quoting a weld repair?
A useful weld repair quote typically needs the original construction code and material specification, the operating and design conditions of the component, the extent and type of damage found during inspection, and any history of prior repairs at the same location. Missing or incomplete records extend the timeline because the material and damage type have to be verified before a repair method can be selected.
Is a weld repair classified as a repair or an alteration under code?
Under codes like API 510 and API 570, a repair restores equipment to its existing design conditions, while an alteration changes them, such as adding a nozzle or increasing the maximum allowable working pressure. A weld repair that only restores the original condition is a repair; if it changes the equipment’s rated capacity or configuration, it is an alteration and requires a more extensive engineering review and code documentation.
Get a Repair vs. Replacement Decision Backed by Testing
Deciding between weld repair and replacement is easiest when it is backed by actual data on the damage, not a guess. WH Labs can evaluate the component, run the testing that supports the decision, and carry out the repair itself once the path forward is clear. Get a Free Quote to have WH Labs evaluate your next weld repair or replacement decision.